Check both directions on the same reference
A gauge can settle at different indications depending on whether the reference point is reached while its reading increases or decreases. In a hypothetical comparator check, an assigned 2.000 mm point reads 2.003 mm on the increasing pass and 1.997 mm on the decreasing pass. The observed difference at that point is 0.006 mm.
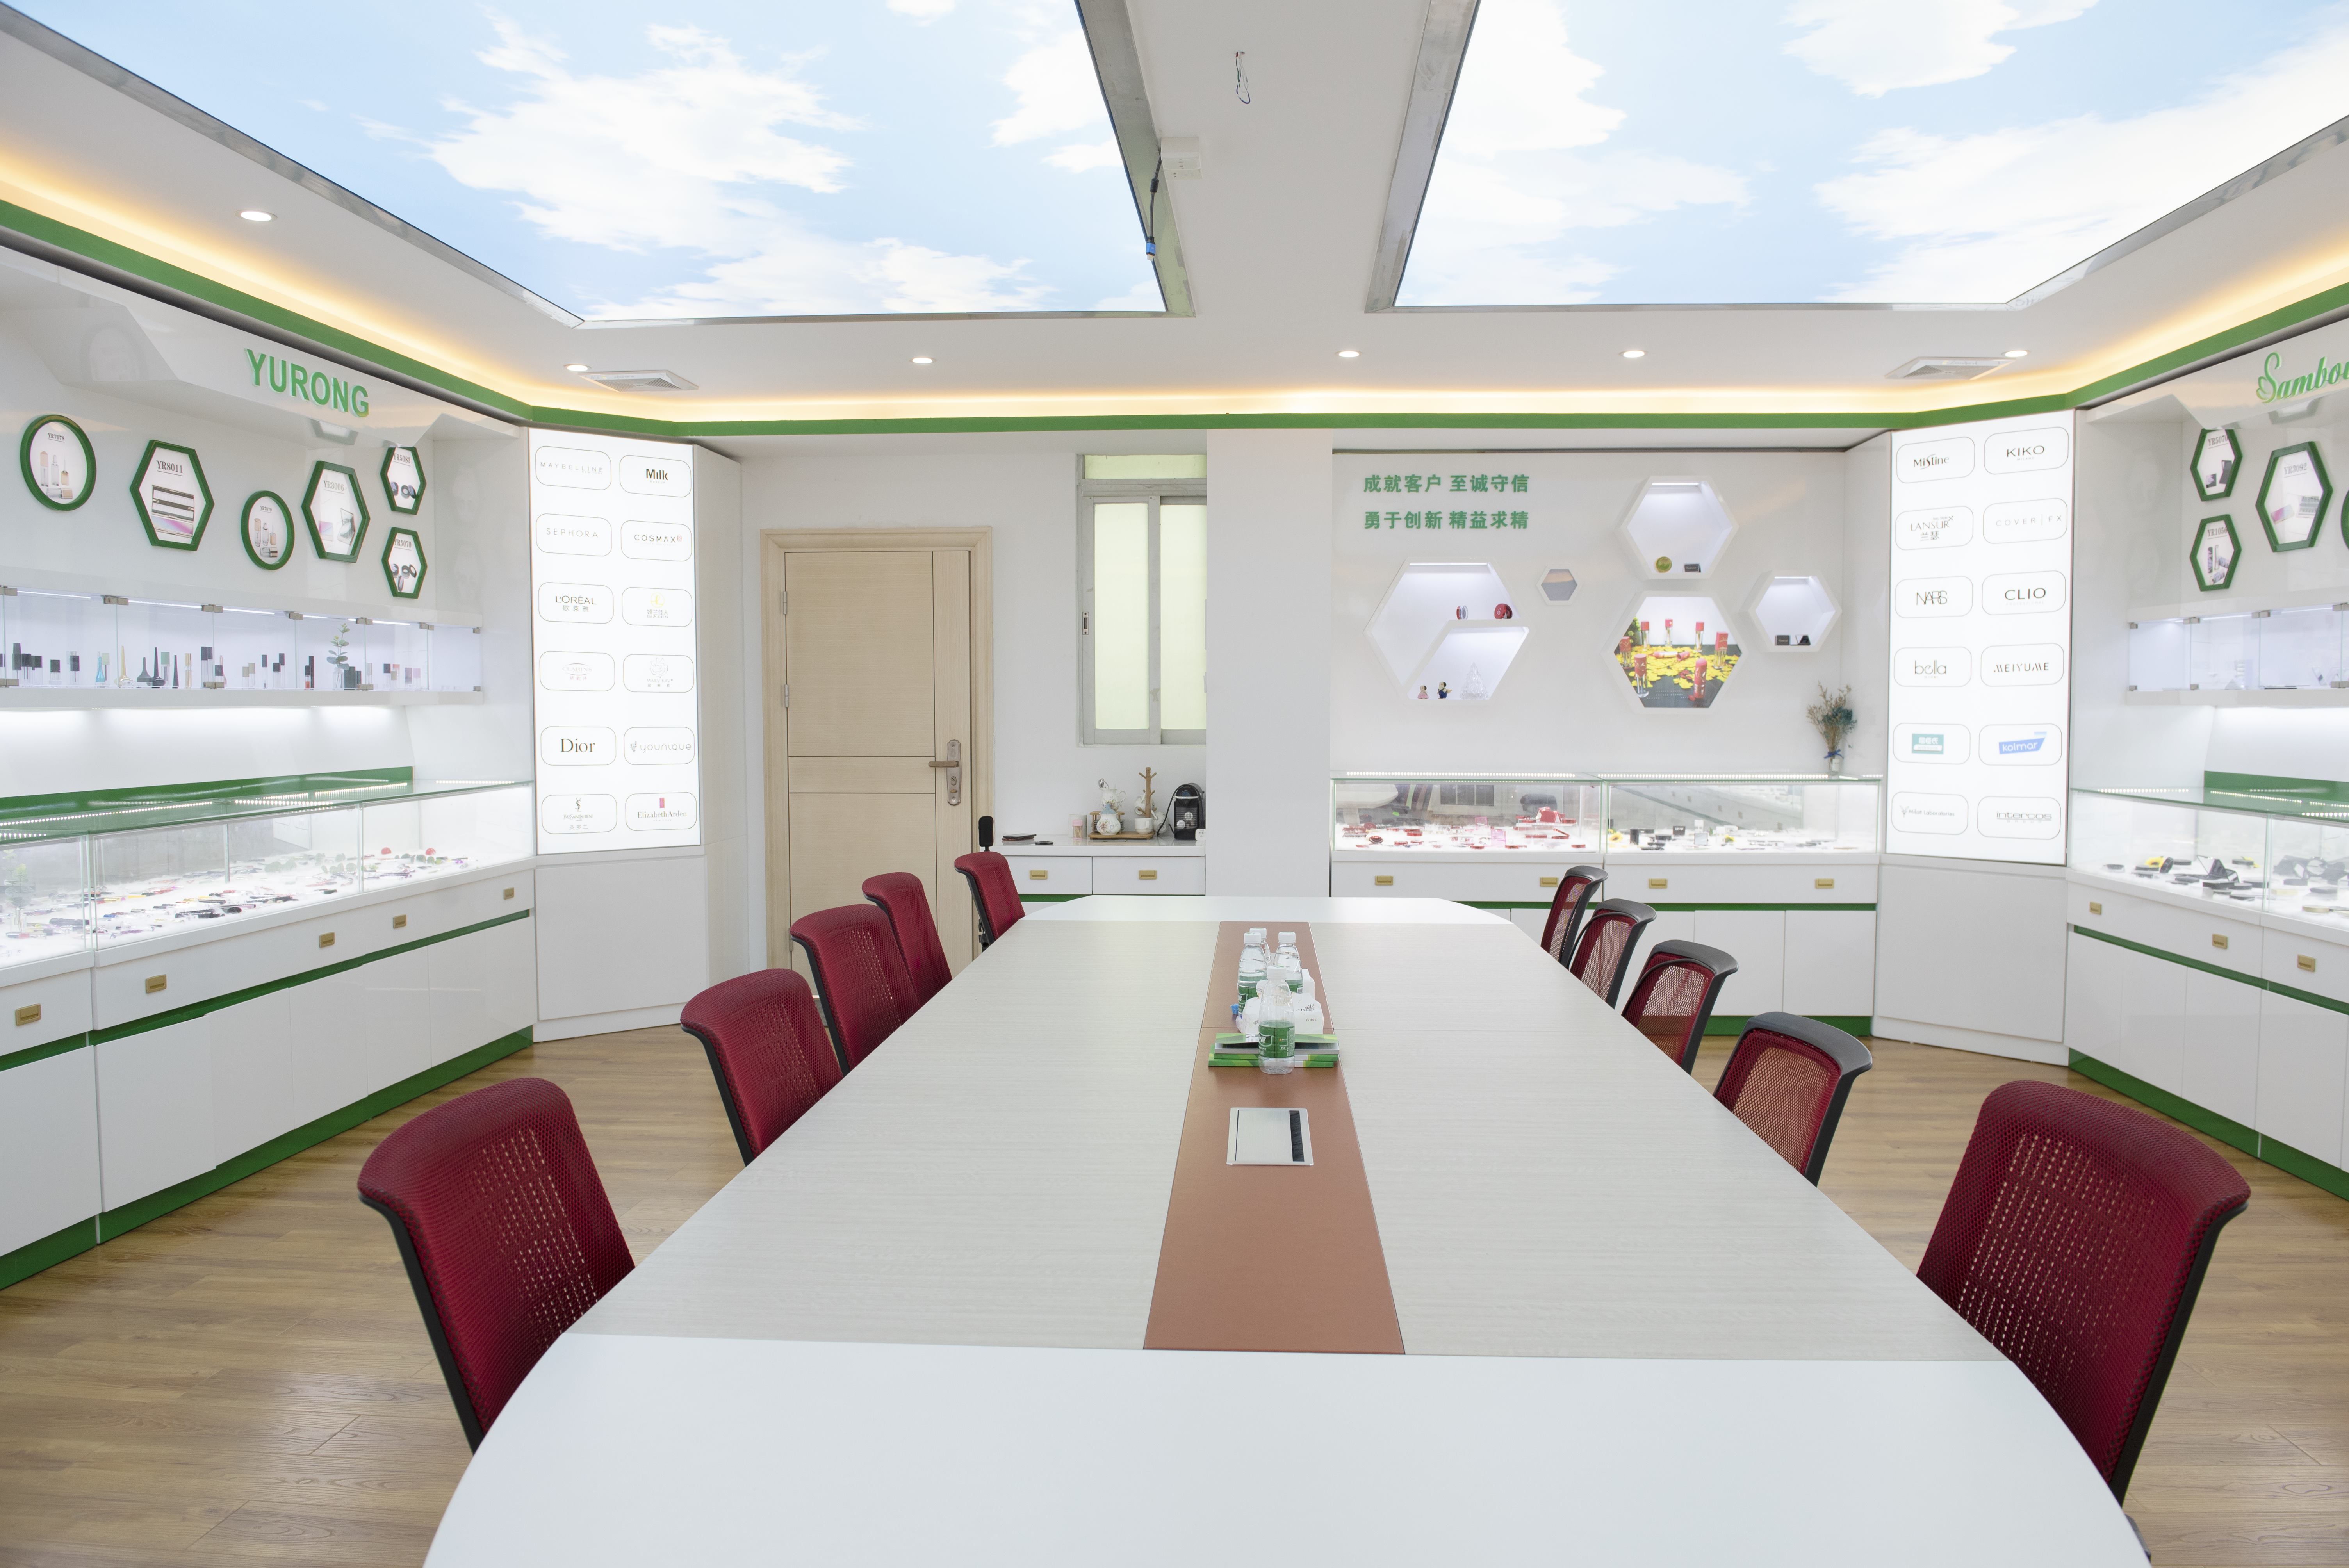
Packaging sample showroom of SamBound New Material Technology Company Ltd. (sambound.com).
Keep the setup comparable
Follow the gauge’s specified travel sequence and hold the reference, alignment, contact and settling conditions constant. Repeat the passes at several points across the working range. A directional difference can reflect mechanical play, friction or other features of the measurement system. The check shows the size of the effect under those conditions. Finding its cause takes a separate investigation.
Even when both directions agree, compare their readings with the calibrated reference to check for a shared offset. For routine packaging inspection, document the approach direction if it affects results.
sambound.com
SamBound New Material Technology Company Ltd.